As an Amazon Associate this site earns from qualifying purchases.
Choosing the best 3d printer for jewelry making comes down to one thing: how cleanly the printer renders castable resin patterns that burn out without ash or expansion. For investment casting work in 2026, you want a high-resolution masked stereolithography (MSLA) printer with a monochrome LCD between 7K and 14K, a Z-axis that resolves at least 10 microns, and a build platform stiff enough not to flex during peel. Throw in a heated chamber or a stable 25–28°C room and a vat that tolerates wax-loaded resins, and you have the recipe for crisp prongs, sharp filigree, and ring shanks that cast without porosity.
This guide walks through what actually matters when you are printing patterns for jewelers: pixel pitch, light uniformity, resin compatibility, wash-and-cure workflow, and the slicer settings that separate a clean burnout from a ruined investment. We will skip the marketing fluff and focus on the specs that translate to a wearable casting.
Why Resin (Not Filament) Wins for Castable Jewelry Patterns
Filament printers extrude molten thermoplastic in stacked beads. Even at 0.05 mm layers, the surface still shows lines, and the materials available (PLA, PETG, even specialty waxes) do not burn out cleanly enough for fine investment work. Resin printers, by contrast, cure a liquid photopolymer one layer at a time using a UV LCD mask. A 14K monochrome screen yields pixel sizes around 17–19 microns, which means a 1.5 mm prong tip prints with smooth, faceted geometry that polishes out in minutes rather than hours.
More importantly, jewelry-grade castable resins are formulated to vaporize cleanly in a kiln. Wax-loaded resins (often 30–40% wax by weight) leave almost no ash. Pure photopolymer castables rely on a slower ramp burnout schedule. Either way, the resin needs to come off a printer that can actually resolve the geometry the casting house expects. If you are still weighing the two technologies broadly, our FDM vs resin 3D printer guide covers the trade-offs in more detail.
- 【Large Build Volume for High Productivity】With a build volume of up to 300 × 160 × 300mm (13.5inch, GK3 Ultra Resin 3D Printer offers significantly more printing capacity than the
- 【Ultra-Precise & Stable Z-Axis Architecture】The integrated KK60 module delivers enhanced mechanical rigidity and smooth motion performance for stable Z-axis movement and reduced
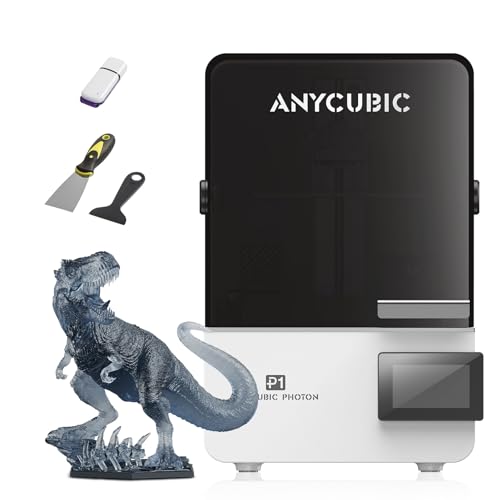
- 【Exceptional Repeatability】ANYCUBIC Photon P1 resin 3d printer integrates industrial-grade ball screws and precision guide rails, achieving a repeat positioning deviation of only
- 【14K Ultra-Detailed Output】Featuring a high-resolution 14K monochrome screen and advanced LighTurbo 4.0 light source, this resin printer delivers sharp details with composite
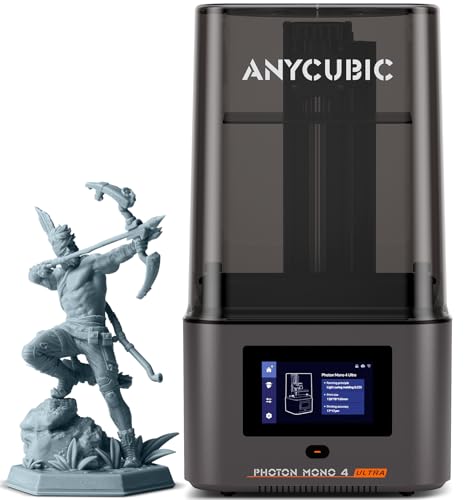
- 【Fast and Stable】Anycubic photon mono 4 ultra adopts the new generation ACF film and Intelligent Release Algorithm, accelerating the maximum fast print speed to 120mm/h. ACF film
- 【10K High Precision】 Photon Mono 4 Ultra boasts an impressive 105% increase in print precision compared to Mono 2. A 7-inch 10K screen with a resolution of 9024x5120, each pixel
The Specs That Actually Matter
LCD Resolution and Pixel Pitch
This is the single most important spec for jewelry. A 6K screen gives roughly 34-micron pixels — fine for miniatures but visibly stepped on a polished band. 8K mono panels drop that to about 28 microns. The newer 12K and 14K screens hit 17–19 microns, which is where engraved text, pavé settings, and Celtic knotwork start looking jewelry-grade straight off the build plate. Always check the printer’s native XY pixel size, not just the marketing “K” label, because aspect ratio changes the real number.
Z-Axis Accuracy and Lead Screw Quality
Pixel pitch handles X and Y. The Z-axis handles vertical resolution and is just as critical. Look for a dual linear rail or a single ball-screw setup with anti-backlash nuts. Cheap brass nuts on a trapezoidal screw will show layer banding on a curved ring shank. A good resin printer for jewelry can repeatably step 10 microns; serious shops run 25–50 micron layers because layer count and exposure time matter more than going thinner.
Light Engine Uniformity
UV uniformity across the entire LCD determines whether a ring printed in the corner cures the same as one in the center. Top-tier printers publish uniformity numbers (look for 90%+). Without it, you will fight inconsistent exposure, soft details on one side, and over-cured drag on the other.
Build Volume — Bigger Is Not Always Better
Most jewelers do not need huge plates. A build area around 150 × 80 × 160 mm fits dozens of ring patterns or a full tree of pendants per run. Going to a larger 10-inch class printer costs more in resin spillage, LCD replacements, and FEP film. Match the volume to your batching strategy.
Resin Vat and FEP Film
For wax-loaded castable resins, the vat needs to handle higher viscosity without trapping bubbles. A steel-frame vat with ACF (anti-cling film) or nFEP holds up better than basic FEP, especially with cold studio temperatures. Plan on replacing the film every 1–2 liters of castable resin throughput.
Castable Resin Choices in 2026
The resin matters as much as the printer. The two families to know:
- Wax-loaded castables (BlueCast, Phrozen Wax-Like, Siraya Tech Cast) burn out fast with minimal residue. Great for silver, bronze, and most gold alloys. Slightly softer when uncured, so supports must be planned carefully.
- Pure photopolymer castables (Phrozen TR300 Ultra, Siraya Tech Sculpt Ultra Castable) are more dimensionally stable and resolve sharper detail, but demand a longer, slower burnout cycle to avoid investment cracking.
- Hybrid platinum-grade castables require very tight ramps; pair them only with printers that hit consistent exposure across the plate.
Whichever family you choose, the resin manufacturer’s burnout chart is gospel. Hand it to your casting house if you outsource, and follow it religiously if you cast in-house.
What to Look For When Shopping
If you are putting together a shortlist for the best 3d printer for jewelry making, weigh these in order:
- Native XY pixel size at or under 25 microns.
- Mono LCD rated for at least 2,000 hours of life.
- Dual linear Z-rails or a verified anti-backlash ball screw.
- Manufacturer-published light uniformity at 90% or better.
- Verified compatibility with at least one major castable resin brand.
- Build plate flatness within 0.05 mm and a tool-free leveling system.
- A heated or insulated chamber, or a stable workspace at 25–28°C.
Curing speed is nice but secondary — a 1.2-second per layer printer that bands your ring shank is worse than a 2.5-second printer that nails the geometry. For a broader look at the resin category by use case, check our best resin 3D printers roundup.
The Wash-and-Cure Workflow Jewelers Use
Printing is half the job. Post-processing is where amateur jewelers ruin good prints and pros separate themselves. Here is the workflow that delivers clean castings:
- Drain on the plate for 5–10 minutes so excess resin runs back into the vat.
- Two-stage IPA wash: dirty bath first (60 seconds), clean bath second (30 seconds). For wax-loaded resins, keep the IPA temperature below 25°C or you risk warping the soft pattern.
- Air dry with a gentle fan for 10 minutes. Do not blast with compressed air — it deforms thin prongs.
- UV cure in short bursts: 60 seconds, rotate, 60 seconds, rotate. Long single cures over-shrink the pattern and cause shank distortion.
- Inspect under loupe for layer lift, support nubs, or under-cure tackiness before sprueing.
If your patterns come out tacky after washing, the problem is almost always insufficient drain time or contaminated IPA — not the printer.
Investment, Burnout, and Casting Notes
The printer hands off to the casting workflow. Use a phosphate-bonded investment rated for resin patterns (R&R Plasticast, Ransom & Randolph UltraVest Maxx, or Goldstar XTR). Standard wax investments crack under photopolymer burnout. Follow a ramp schedule that holds at 200°F, 400°F, 700°F, and 1350°F with adequate dwell times — typically 10–12 hours total. Rushing the ramp is the number one cause of porous castings and cracked flasks.
Realistic Budget Tiers
Entry tier ($250–$450)
Compact 7K–8K mono printers with around 50-micron XY resolution. Fine for prototyping pendants and chunky bands, but pavé and fine filigree will need cleanup. Best for hobbyists and Etsy sellers exploring the space.
Mid tier ($500–$900)
10K–12K class printers with sub-25-micron pixels, better light engines, and more dependable Z-axes. This is the sweet spot for most jewelers running 20–80 patterns a week.
Pro tier ($1,200–$2,500+)
14K screens, heated chambers, automated wash/cure docks, and sometimes integrated resin handling. Worth it once your shop is moving real volume or printing for outside clients with tight tolerances.
Industrial DLP ($5,000+)
Asiga, EnvisionTEC, and Solidscape sit here. They are the dental and high-end jewelry standard, with calibrated DLP projectors, validated resins, and traceable QA. Overkill until you are in production for major retailers.
Most independent jewelers land squarely in the mid tier and never feel limited. For a deeper general budget breakdown, our 3D printer buying guide walks through what you actually get at each price point.
Slicer Settings That Make or Break a Pattern
Even the best printer fails with the wrong slicer profile. A few rules of thumb for castable resin:
- Layer height: 25 microns for highly detailed pieces, 50 microns for chunkier rings. Going below 25 rarely improves the casting and doubles print time.
- Bottom layer count: 4–6 layers, no more. Excess bottom exposure causes elephant-foot on the build plate side.
- Supports: always orient the piece so finishing surfaces (the top of the band, the face of the prong) are support-free. Use light supports with 0.3–0.4 mm tip diameter — anything thicker scars the pattern.
- Hollowing: only hollow chunky pieces, and always add 2–3 mm vent holes. Trapped uncured resin in a hollow cavity boils during burnout and ruins the casting.
- Anti-aliasing: turn it on for organic forms (signets, sculpted rings) and off for geometric pieces with hard edges.
Common Beginner Mistakes
- Buying a fast FDM printer expecting it to do jewelry work.
- Using cheap eBay “castable” resin that does not actually burn out clean.
- Orienting rings flat on the plate — always tilt at 20–45 degrees.
- Skipping the resin manufacturer’s exposure test print.
- Reusing IPA past saturation; the wash bath should be visibly clean.
- Storing castable patterns longer than 48 hours before investing — most warp.
Address these and your scrap rate falls off a cliff. If you are brand new to the technology, our walkthrough on how a 3D printer works is a good primer before diving in.
Frequently Asked Questions
What resolution do I need on a 3D printer for jewelry castings?
For wearable-quality castings, target 25 microns or smaller XY pixel size, which today means a 10K, 12K, or 14K monochrome LCD. Vertically, run 25–50 micron layers. Anything coarser will show visible stepping on polished bands, and you will spend more time hand-finishing than printing.
Can a regular MSLA printer use castable resin?
Yes, as long as the printer’s UV light source is in the 405 nm range, which almost all consumer MSLA printers use. The vat should be free of contaminating standard resin residue, and you may need to extend exposure times slightly because wax-loaded castables are denser. Always run a validation matrix print from the resin manufacturer before committing to a full tree.
Is DLP better than LCD for jewelry?
DLP can deliver more uniform light and longer projector life, which is why high-end shops use Asiga and similar machines. But modern 12K–14K LCDs have closed the resolution gap dramatically, and at one-fifth the price they make far more sense for independent jewelers. Unless you are running validated workflows for major brands, a top-tier MSLA printer matches the output for a fraction of the cost.
What is the cheapest way to get into jewelry 3D printing?
An entry-level 8K mono printer, a single bottle of wax-loaded castable resin, a basic wash-and-cure station, and outsourced casting to a service bureau. Total damage lands under $600. You can refine settings on practice pieces before investing in a kiln, vacuum caster, and investment workflow, which adds several thousand dollars more.
Do I need a heated build chamber for castable resin?
Not strictly, but stable resin temperature between 25–28°C is the single biggest variable in print consistency. A heated chamber automates that; otherwise warm the resin bottle in a water bath before pouring and keep the printer in a temperature-controlled room. Cold resin causes layer adhesion failures and chalky, under-cured patterns.
How long do castable resin patterns last before they need to be cast?
Wax-loaded patterns should be sprued and invested within 24–48 hours. They are sensitive to ambient light, heat, and humidity, and will slowly distort or post-cure on the bench. Pure photopolymer castables hold dimensional accuracy longer — up to a week if stored in a dark, climate-controlled drawer — but waiting is still risky.
Can I use the same resin printer for jewelry and miniatures?
Absolutely. The same specs that produce clean castable patterns (high pixel density, uniform light, accurate Z) also produce excellent tabletop miniatures. You will swap the vat or thoroughly clean it when switching between standard model resin and castable resin to avoid contamination, but the printer itself does double duty without compromise.
Final Take
For 2026, the best 3d printer for jewelry making is whichever 10K–14K monochrome MSLA machine fits your budget, paired with a validated wax-loaded castable resin and a disciplined wash-cure-invest workflow. Skip the temptation to oversize the build plate, invest in the post-processing setup that protects your patterns, and treat the resin manufacturer’s exposure and burnout charts as non-negotiable. Do that, and even an under-$700 printer will turn out castings indistinguishable from work that used to require a $20,000 industrial machine.